Foam density
25D EVA compresses around a device and absorbs shock; 38D EVA holds a shaped cavity flat under a 2 kg tool. Both are laminated to 1680D nylon or jersey in-house.
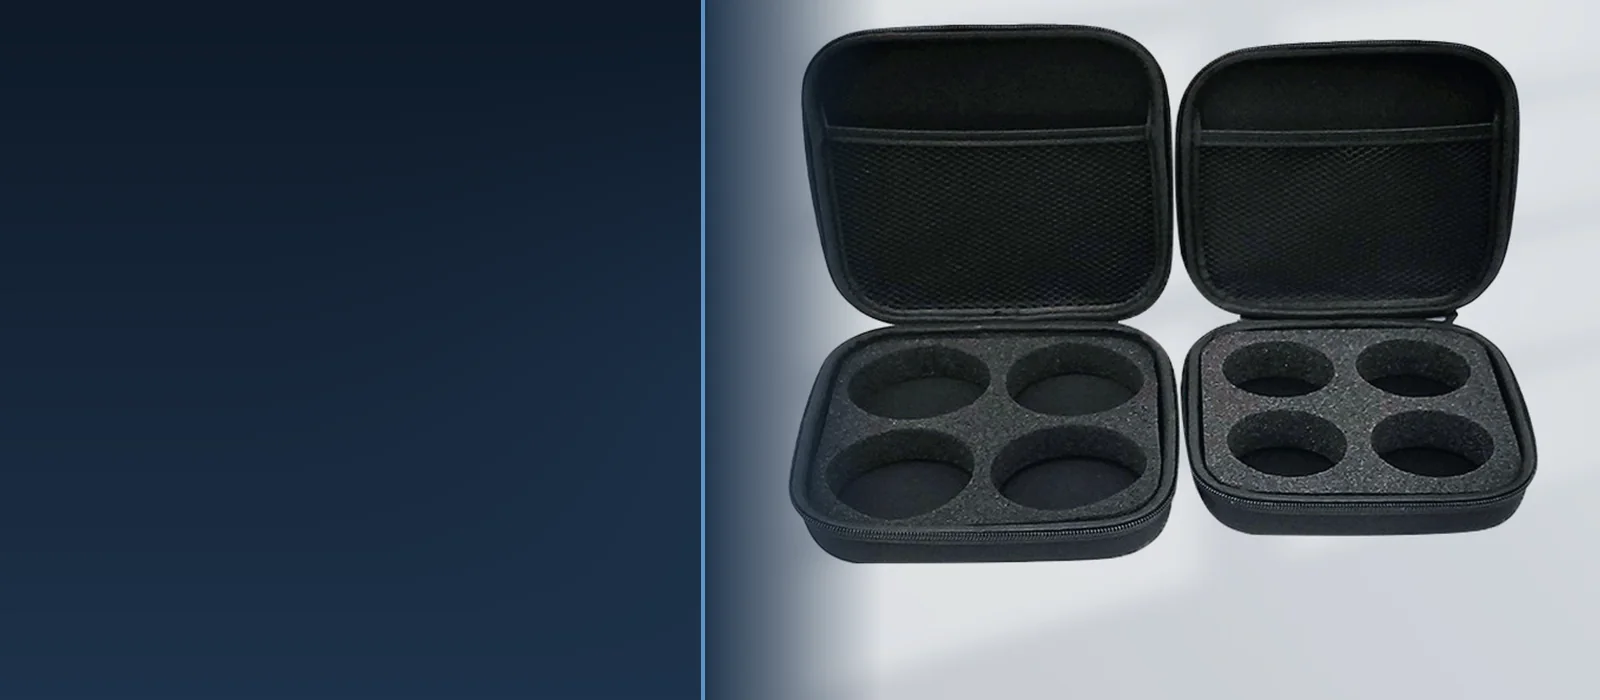
A foam insert turns a moulded shell into a case that holds one device, in one orientation, with the lid closing on the same tolerance every time. We cut four insert types in Shijie Town: die-cut EVA, pick-and-pluck foam, thermoformed EVA trays and moulded EVA shells. This page compares what each costs, how precise it is, and which quantity justifies the tooling.
An insert starts with the device, not the case. We ask for the unit itself, a 1:1 mock-up, or a STEP file with the ports, buttons and antenna zones marked. From that we set the cavity, the finger pull and the lid clearance. Die-cut EVA holds ±2 mm on the outline, so a phone-sized cavity is easy and a 90 mm lens barrel needs a test cut before bulk.
Density decides how the insert behaves in a drop test. A 25D EVA at 20 mm cushions the device and absorbs a 1.2 m drop, but it sags under a 2 kg tool. A 38D EVA at 15 mm stays flat and holds a shaped cavity without a backing board. Most cases we build use 25D on the lid and 38D in the base.
Change one and the unit moves inside the shell. We fix all three before a die is made.
25D EVA compresses around a device and absorbs shock; 38D EVA holds a shaped cavity flat under a 2 kg tool. Both are laminated to 1680D nylon or jersey in-house.
Inserts run 10–30 mm. A 10 mm sheet lines a lid, 20 mm cradles a camera body, 30 mm fills a tool case. Shell depth, not foam size, sets the limit.
Die-cut EVA holds ±2 mm on the cavity edge. Pick-and-pluck holds ±5 mm because it releases in 10 mm squares. Give us the device tolerance and we pick the process.
Every insert is checked against the device, not the drawing. We cut a first article, load the actual unit, close the shell and shake it. A 90 mm lens barrel should not shift; a 12 mm cable channel should still pass a plug. Any cavity outside ±2 mm goes back to the CAD table before the die is cut and the drawing is reissued.
Foam is tested as an assembly, because a case only protects as a stack. We drop 1.2 m on six faces with the device loaded, compress a 20 mm insert to 50% of its height for 1,000 cycles, and measure how much it recovers. An insert that loses more than 3 mm is re-cut in 38D. Density and phthalate test reports are available on request.
Each photo is a production insert, not a render. Every one can be re-cut for your device.
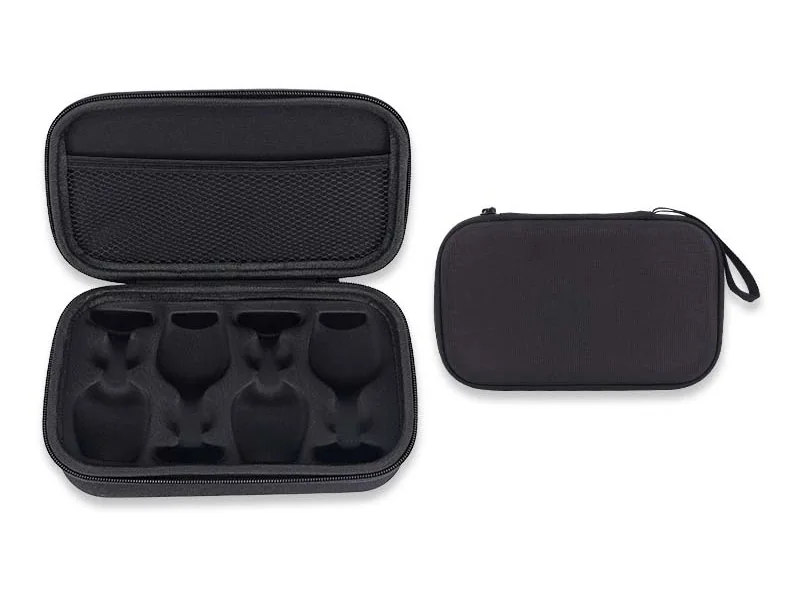
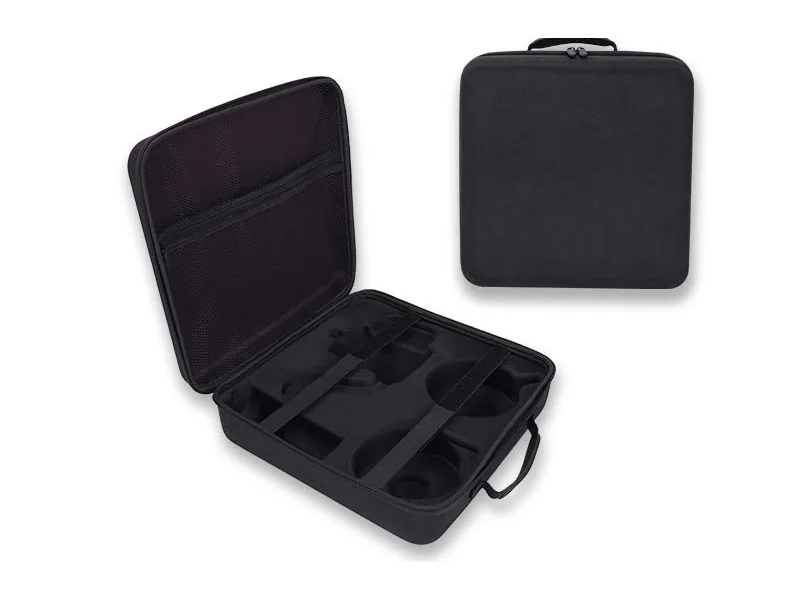
38D base, ±2 mm cavity, drone body
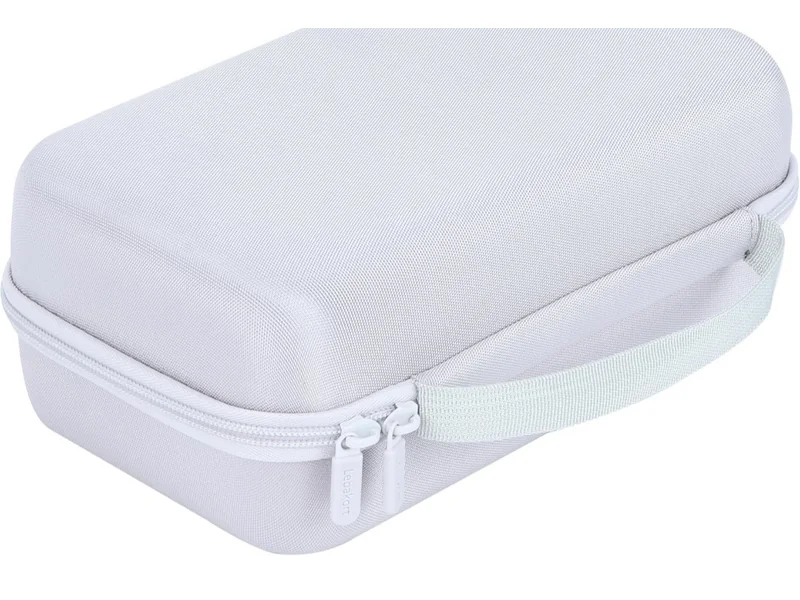
30 mm pre-cut grid, camera kit, 100 pcs
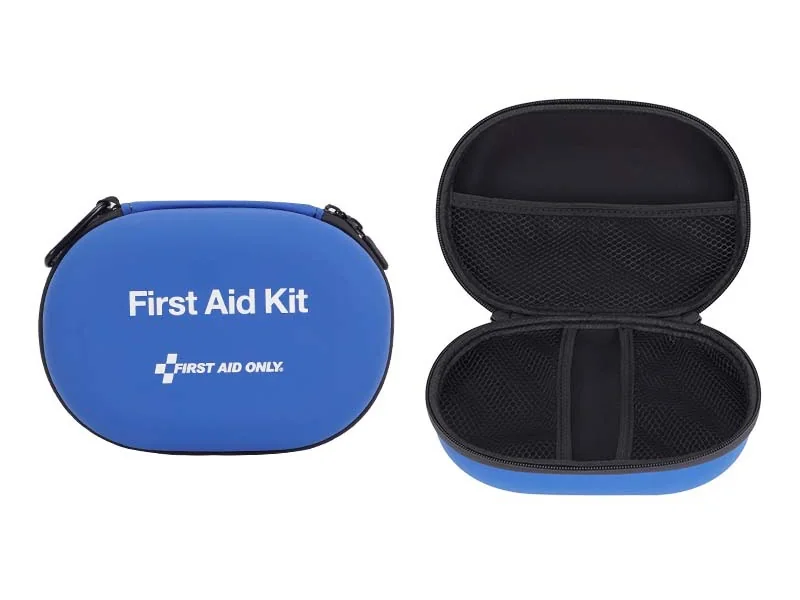
1 mm tray, VR headset, drop-in fit
5 mm 75D shell, shaped tool cavity
Most insert projects take 20–40 days end to end, depending on whether a die has to be made.
Ship the unit, or send a STEP file with ports and buttons marked. A photo plus three measurements is enough for an indicative quote in 2 working days.
We match the device, the quantity and the budget to one of the four insert types, then confirm the cavity drawing within 2 working days.
We cut one insert, load the device and send photos with the cavity measurements. You approve the fit before the die is ordered or the run goes ahead.
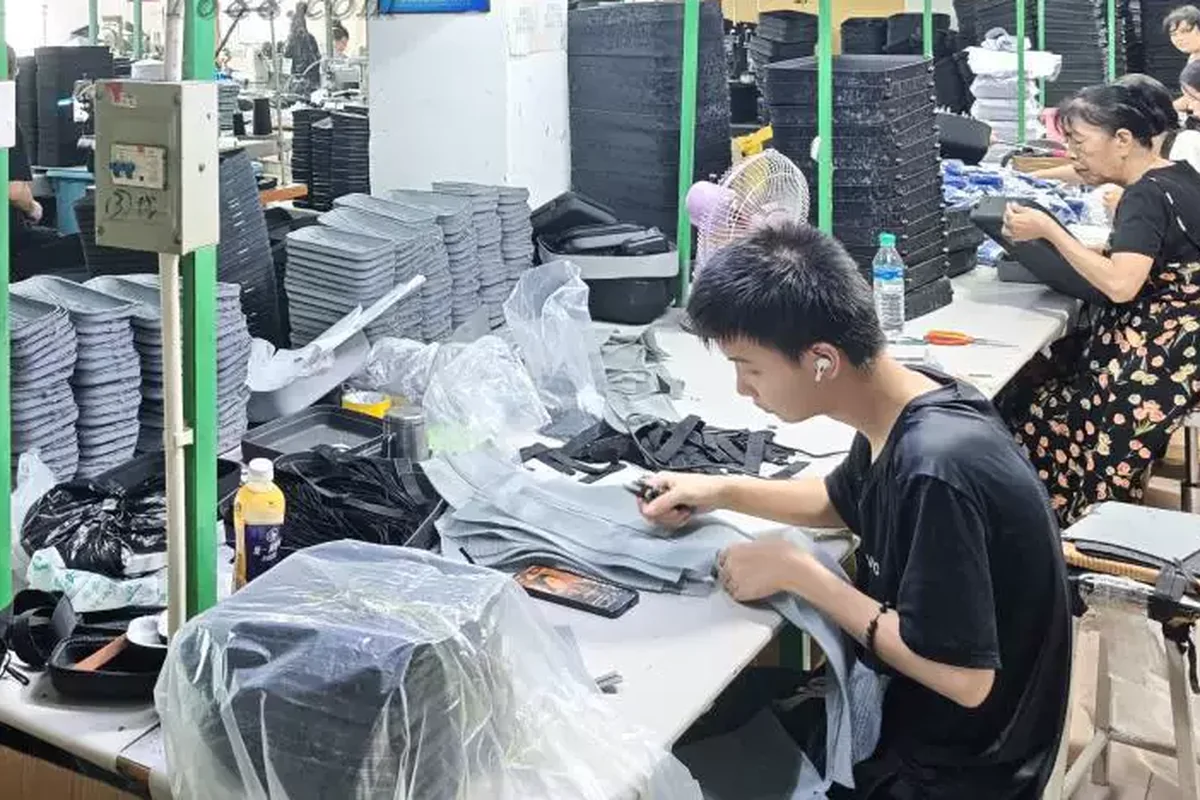
Die-cut and pick-and-pluck inserts run at 500–1,000 pcs a day, laminated to the shell lining with hot-melt film and checked at every 20th piece against the drawing.
Inserts ship flat or pre-fitted in the case, polybagged at 25 pcs per carton with a packing list, FOB Shenzhen or Yantian, CIF or DDP.
Tooling, tolerance and minimum run separate these four. Each can be laminated to velvet, jersey or 5 mm EVA.
Pick by quantity first, then by how precisely the device seats in the cavity.
A steel-rule die cuts the cavity in one stroke, so every piece matches to ±2 mm. The tool is a one-off, so the process makes sense above 500 pcs. Clean edges, no grid.
Pre-cut foam releases in 10 mm squares, so the cavity is shaped by hand. No tool, so a 100 pcs run is possible. Edges are stepped and the fit is ±5 mm.
A heated 1 mm EVA sheet is pulled over a former, giving thin walls and a repeatable drop-in fit. The choice when a device has to seat the same way every time.
The 5 mm case wall is compressed around a shaped cavity, so there is no separate insert. The strongest build, needs a steel mould, and pays back at 2,000 pcs.
FOB Shenzhen, 1,000 pcs unless the line states otherwise, insert fitted and shell lined. New dies and moulds are quoted separately.
US$2.90 / pc
100–499 pcs, medium stock shell, 30 mm pluck foam, your logo on the lid.
US$4.60 / pc
500–1,999 pcs, die-cut 38D insert with a ±2 mm cavity, velvet lining.
US$8.40 / pc
2,000+ pcs, new moulded EVA shell with the cavity formed into the wall.
Five questions buyers ask before sending a device outline.
A STEP file, a 1:1 mock-up or the unit itself is enough to start. We reply with an insert type, a tolerance and a price.